In the modern chemical processing landscape, organic solvents serve as the essential lifeblood of operations. From the synthesis of active pharmaceutical ingredients (APIs) and semiconductors to high-performance polymers, coatings, and fine chemicals, solvents are indispensable for reaction media, purification, and equipment cleaning. However, the traditional line of solvent consumption follows a linear "take-make-dispose" model, where vast quantities of high-purity solvents are consumed once and sent off-site for hazardous waste incineration or land disposal.
Today, volatile energy markets, strict environmental regulations, and volatile raw material supply chains have made solvent disposal a major financial burden and environmental liability. Industrial plant managers, process engineers, and sustainability leads are actively seeking methods to close the loop on solvent streams.
Solvent recovery and recycling represents a major decarbonization and cost-reduction opportunity in industrial processing. By integrating advanced separation technologies, ranging from traditional thermal distillation to breakthrough, pressure-driven Organic Solvent Nanofiltration (OSN), chemical manufacturers can recover up to 95% of spent organic solvents on-site, re-introducing technical-grade and high-purity solvents back into production lines at a fraction of the original cost and carbon intensity.
This guide explores industrial solvent recycling for the specialty chemicals sector, examining economic benefits, technical mechanisms, comparison of technologies, and actionable evaluation frameworks for choosing the ideal recovery system.
Why Solvent Recovery Matters in the Specialty Chemicals Industry
Specialty chemical manufacturing is characterized by low-volume, high-value production processes that require specialized solvent chemistry. Unlike commodity chemicals, specialty chemical manufacturing often relies on complex, expensive, and frequently toxic solvents.
Several macroeconomic and regulatory forces are driving the shift toward on-site solvent recovery:
1. High Raw Material Volatility and Supply Chain Risks
Petroleum-derived organic solvents are subject to global supply chain disruptions and volatile commodity pricing. In reliance on off-site suppliers, facilities face unpredictable lead times and escalating procurement expenditures. Reclaiming spent solvents on-site shields plants from raw material price shocks and secures a stable internal supply.
2. Escalating Hazardous Waste Disposal Costs
Disposing of spent organic solvents is an expensive operating expense. Transportation regulations for hazardous materials, regulatory compliance paperwork, and off-site tipping or incineration fees have increased significantly. Facilities paying twice, first to buy virgin solvent, then to dispose of contaminated waste, face compounding operational expenses.
3. Stringent Environmental Regulations and Decarbonization Targets
Global regulatory bodies and regional environmental protection agencies, continue to tighten limits on Volatile Organic Compound emissions, hazardous waste generation, and industrial effluent. Furthermore, corporate Environmental, Social, and Governance (ESG) commitments demand tangible reductions in greenhouse gases.
What Are the Main Benefits of Using Solvent Recovery Systems in Industrial Processes?
In the modern chemical processing landscape, organic solvents serve as the essential lifeblood of operations. From the synthesis of active pharmaceutical ingredients (APIs) and semiconductors to high-performance polymers, coatings, and fine chemicals, solvents are indispensable for reaction media, purification, and equipment cleaning. However, the traditional line of solvent consumption follows a linear "take-make-dispose" model, where vast quantities of high-purity solvents are consumed once and sent off-site for hazardous waste incineration or land disposal.
Today, volatile energy markets, strict environmental regulations, and volatile raw material supply chains have made solvent disposal a major financial burden and environmental liability. Industrial plant managers, process engineers, and sustainability leads are actively seeking methods to close the loop on solvent streams.
Solvent recovery and recycling represents a major decarbonization and cost-reduction opportunity in industrial processing. By integrating advanced separation technologies, ranging from traditional thermal distillation to breakthrough, pressure-driven Organic Solvent Nanofiltration (OSN), chemical manufacturers can recover up to 95% of spent organic solvents on-site, re-introducing technical-grade and high-purity solvents back into production lines at a fraction of the original cost and carbon intensity.
This guide explores industrial solvent recycling for the specialty chemicals sector, examining economic benefits, technical mechanisms, comparison of technologies, and actionable evaluation frameworks for choosing the ideal recovery system.
Why Solvent Recovery Matters in the Specialty Chemicals Industry
Specialty chemical manufacturing is characterized by low-volume, high-value production processes that require specialized solvent chemistry. Unlike commodity chemicals, specialty chemical manufacturing often relies on complex, expensive, and frequently toxic solvents.
Several macroeconomic and regulatory forces are driving the shift toward on-site solvent recovery:
1. High Raw Material Volatility and Supply Chain Risks
Petroleum-derived organic solvents are subject to global supply chain disruptions and volatile commodity pricing. In reliance on off-site suppliers, facilities face unpredictable lead times and escalating procurement expenditures. Reclaiming spent solvents on-site shields plants from raw material price shocks and secures a stable internal supply.
2. Escalating Hazardous Waste Disposal Costs
Disposing of spent organic solvents is an expensive operating expense. Transportation regulations for hazardous materials, regulatory compliance paperwork, and off-site tipping or incineration fees have increased significantly. Facilities paying twice, first to buy virgin solvent, then to dispose of contaminated waste, face compounding operational expenses.
3. Stringent Environmental Regulations and Decarbonization Targets
Global regulatory bodies and regional environmental protection agencies, continue to tighten limits on Volatile Organic Compound emissions, hazardous waste generation, and industrial effluent. Furthermore, corporate Environmental, Social, and Governance (ESG) commitments demand tangible reductions in greenhouse gases.
What Are the Main Benefits of Using Solvent Recovery Systems in Industrial Processes?
Integrating modern solvent recycling into specialty chemical processing offers several distinct advantages:
1. Significant Energy Savings and Carbon Reduction
By replacing fossil-fuel-driven steam boilers with pressure-driven membrane filtration, plant managers can cut energy consumption associated with solvent recovery by up to 90%. This directly advances facility-wide net-zero initiatives and decarbonization roadmaps.
2. High Recovery Yields and Technical-Grade Purity
Advanced OSN membranes retain multivalent ions, organometallic catalysts, fine particulates, and unreacted monomers, yielding clear, high-purity solvents ready for immediate re-use in reaction or washing steps.
3. Process Intensification and Circular Cascade Reuse
Recovered solvents can either be looped directly back into the primary synthesis step or cascaded into secondary washing, vessel cleaning, or lower-grade technical applications, establishing a closed-loop circular economy on-site.
4. Preservation of Heat-Sensitive Compounds
In pharmaceutical synthesis, natural product extractions, and fine chemical processing, active molecules degrade under heat. Cold, membrane-based recovery preserves high-value solute integrity within the retentate stream while purifying the solvent permeate.
5. Footprint Efficiency and Modular Scalability
Membrane systems feature a small physical footprint compared to tall distillation columns. Modular skid designs allow facilities to scale recovery capacity incrementally as production volumes grow.
What Should I Consider When Choosing a Solvent Recovery Machine or System for My Business?
Selecting the optimal solvent recovery system requires evaluating process chemistry, engineering parameters, and financial objectives.
When specifying a recovery system, chemical engineers and plant operators should assess the following key factors:
1. Chemical Compatibility and Membrane Durability
Verify that the recovery system can handle aggressive organic solvents without material degradation. Polymer seals, gaskets, and membrane materials must resist swelling, dissolution, or chemical attack when exposed to aggressive solvents.
2. Energy Availability and Facility Infrastructure
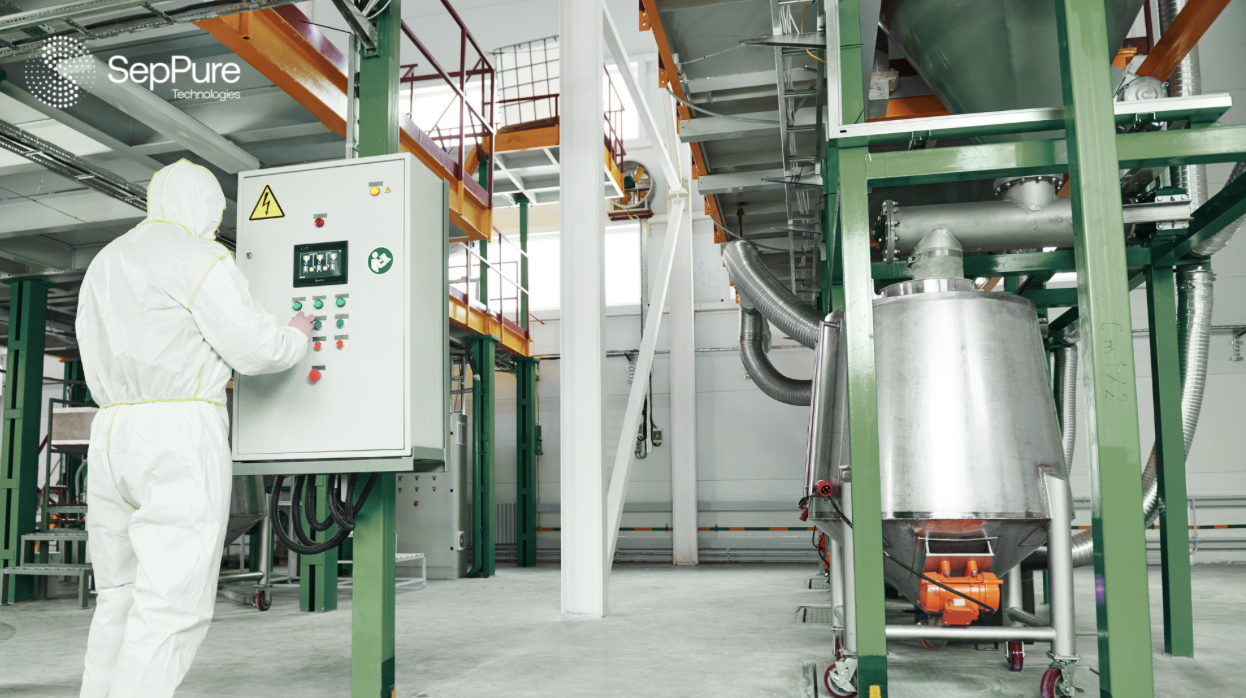
Thermal systems require steam boilers, cooling towers, and heavy electrical infrastructure. If facility thermal utilities are constrained or at capacity, pressure-driven OSN systems offer a plug-and-play alternative requiring only electrical pump power.
3. Regulatory Compliance and Hazardous Location Certification
Solvent recycling units installed on the plant floor must comply with local safety standards, including ATEX, IECEx, or NFPA Class I, Division 1/2 explosion-proof ratings for handling flammable solvents safely.
4. Total Cost of Ownership & CAPEX vs. OPEX Models
Evaluate total operational expenses including energy usage, maintenance, membrane replacement intervals, and labor. Consider flexible commercial models, such as SepPure's zero-CAPEX performance model, which aligns technology adoption with operational savings.
Can Solvent Recycling Help Reduce Environmental Impact and Waste Management Costs?
Yes. Solvent recovery delivers immediate, dual-bottom-line benefits by lowering environmental impact and operating costs.
Environmental Impact Reduction
Substantial Carbon Footprint Reduction: Burning waste solvent via off-site thermal incineration releases significant amounts of CO₂ directly into the atmosphere. Recycled solvents avoid both incineration emissions and the upstream carbon intensity associated with synthesizing new virgin chemicals.
Minimized Emissions: Eliminating the transportation of hazardous waste tanker trucks reduces indirect supply chain emissions.
Conservation of Fossil Feedstocks: Reusing organic molecules directly reduces petroleum extraction and chemical refining burdens.
Financial and Operational Cost Savings
Direct Solvents Procurement Savings: By reclaiming 80% to 95% of solvents on-site, virgin purchasing volumes drop dramatically.
Elimination of Waste Haulage Costs: Waste streams requiring specialized off-site treatment decrease by up to 90%, yielding operational cost savings.
Rapid ROI and Flexible CAPEX Models: Modern solvent recycling solutions provide short payback periods (often under 12 to 18 months). Furthermore, advanced providers like SepPure Technologies offer zero-CAPEX, service-based payment structures where facilities pay based on the tonnage of solvent recovered, removing financial barriers to entry.
Which Solvents Can Be Recovered and Recycled in Specialty Chemicals?
Specialty chemical processing, spanning performance polymers, electronic chemicals, agrochemical active ingredients, and fine chemical synthesis, relies heavily on complex, high-cost organic solvents. Unlike commodity chemical manufacturing, which often uses simple aliphatic streams, specialty chemistry routinely employs aggressive polar aprotic media, specialized ethers, and fluorinated compounds for high-yield reaction steps and precise extractions.
Virtually all major organic solvent classes used across specialty chemical reaction steps, catalyst washes, crystallizations, and equipment rinsing can be recovered on-site and restored to technical-grade purity. Modern separation technologies handle the distinct challenges posed by each specific chemical class:
Polar Aprotic Solvents: These solvents are foundational for nucleophilic substitutions, peptide synthesis, lithium-ion battery slurry preparation, and semiconductor wafer stripping. Because they feature exceptionally high boiling points, traditional thermal distillation requires immense energy and frequently causes solvent degradation or discoloration. Non-thermal Organic Solvent Nanofiltration (OSN) is uniquely suited for these high-value streams because it separates contaminants under ambient pressure without heat.
Ethers and Cyclic Ethers: Essential for organometallic reactions, Grignard chemistry, and high-performance polymer synthesis. These solvents present significant thermal hazards due to their tendency to form explosive peroxides when heated during distillation, and they aggressively swell standard polymeric seals. Pressure-driven, ambient-temperature membrane filtration eliminates thermal peroxide risks while reclaiming pure ether streams.
Aromatic Hydrocarbons: Widely used as carrier media for resin synthesis, high-temperature condensations, and homogeneous organometallic catalyst reactions. These aggressive aromatic streams require highly robust, chemically inert membrane materials that cleanly separate the pure aromatic liquid from dissolved high-molecular-weight resins, oligomers, or precious metal catalysts.
Ketones and Esters: Critical for active ingredient crystallization, photoresist formulation, adhesive manufacturing, and fine chemical vessel cleaning. Heat exposure during conventional recovery can trigger thermal degradation, ester hydrolysis, or unwanted side reactions. Cold membrane recovery preserves the chemical stability of the ester or ketone structure.
Specialized Alcohols and Fluorinated Media: Fluorinated solvents are essential in specialized peptide chemistry and advanced fluoropolymer manufacturing, but they can cost upwards. Reclaiming over 95% of these high-cost streams provides near-immediate financial returns, even on small-batch production lines.
How Does a Solvent Recycler Work and What Types of Solvents Can It Handle?
Industrial solvent recycling systems operate by separating pure solvent molecules from non-volatile or molecularly distinct contaminants (such as dissolved solids, resins, active ingredients, heavy oils, polymers, and color impurities).
Historically, this separation has relied on thermal phase changes. Today, membrane-driven molecular filtration offers an alternative mechanism.
1. Thermal Solvent Recyclers (Distillation & Evaporation)
Traditional recyclers heat a contaminated solvent mixture until the solvent reaches its boiling point. The solvent converts into a vapor phase, leaving non-volatile contaminants behind in the boiling chamber. The vapor is then routed to a condenser where it cools back into a liquid state.
Batch Distillation: Solvent waste is heated in a vessel; pure vapor is collected sequentially.
Thin-Film / Wiped-Film Evaporators: Ideal for heat-sensitive or high-viscosity residues, spreading liquid into a thin film along heated walls.
Vacuum Distillation: Lowers the system pressure to reduce the boiling point of high-boiling-point solvents to prevent thermal degradation.
2. Membrane-Based Solvent Recyclers (Organic Solvent Nanofiltration - OSN)
Membrane-based recyclers avoid heating and phase changes. Instead, systems such as SepPure's RE(SOLV)® technology utilize pressure-driven separation through chemically resistant Organic Solvent Nanofiltration (OSN) membranes.
Molecular Size-Exclusion: The waste solvent stream is pressurized across a specialized hollow-fiber or spiral-wound membrane featuring nanometer pores
Selective Permeation: Small solvent molecules permeate freely through the membrane pore structure, while larger dissolved solutes, catalyst residues, dyes, or polymers are retained.
Heatless Operation: Separation occurs entirely in the liquid phase without phase changes, drastically reducing the energy footprint.
Traditional Separation vs. Membrane-Based Solvent Recovery
While thermal distillation has long served as the standard for chemical processing, membrane-based Organic Solvent Nanofiltration (OSN) addresses many of the core operational, economic, and safety limitations of thermal systems.
Key Technological Differentiation: SepPure Technologies
SepPure Technologies has commercialized proprietary chemical-resistant hollow-fiber OSN membranes engineered to operate in harsh polar and polar-aprotic environments. Their systems, marketed under product names like RE(SOLV)® (for solvent recycling) and DE(SOLV)® (for process stream desolvation), achieve solvent purity levels exceeding 99.9% while eliminating thermal infrastructure demands.
Solvent recovery in the specialty chemical industry has evolved from a passive waste management practice into a primary driver of process efficiency, cost optimization, and industrial decarbonization.
While traditional thermal distillation remains a common method, next-generation membrane separation, specifically Organic Solvent Nanofiltration (OSN), delivers higher energy efficiency, superior safety profiles, and lower operating costs. By eliminating the heat requirement from solvent separation, technologies allow chemical manufacturers to recover up to 95% of spent solvents, reduce energy usage by 90%, and build resilient, sustainable chemical manufacturing operations.